 You are here:
Automatic Blind Rivet Machine Types: Handheld to Robotic Cells
What Are the Types of Automatic Blind Rivet Machine? Handheld, Fixed, Dual-Gun and Robotic Cells Compared
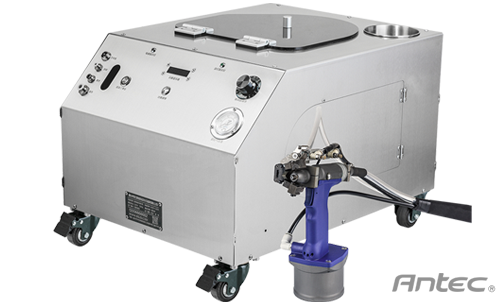
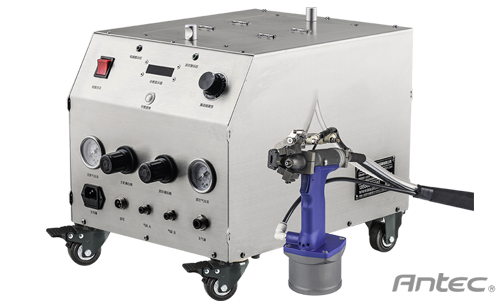
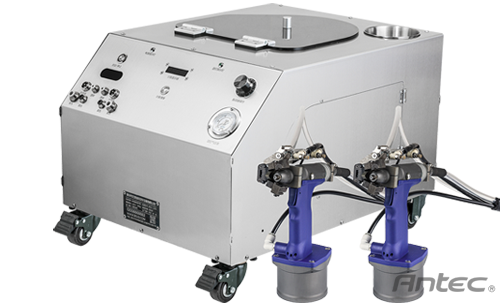
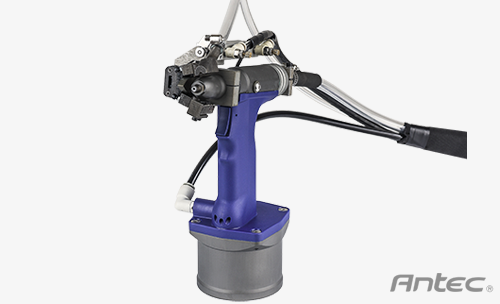
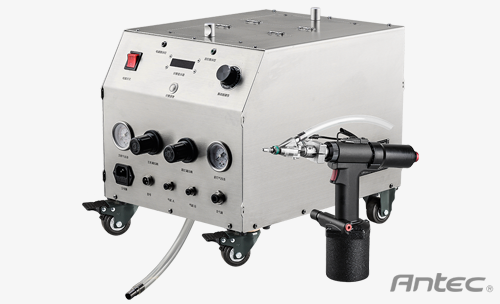
Automatic blind rivet machines fall into four groups by form factor and degree of automation: the handheld automatic rivet gun, the bench or fixed model, the dual-gun model (one machine, two guns) and the robotic riveting cell. These are not stacked quality tiers; each matches a different product structure, output level and stage of investment. Here is how they differ, with a selection path at the end.
1. The Four Types Side by Side
| Type | How it works | Where it fits | Strengths |
|---|---|---|---|
| Handheld automatic rivet gun | Operator moves the gun to the work; the power unit feeds rivets automatically | Large parts, scattered rivet points, high-mix low-volume | Flexible, lowest investment, quick to learn |
| Bench / fixed | Part is located on a worktable or fixture while the gun works in place | Small parts, fixed station, dense rivet patterns | Good consistency, takes fixtures well |
| Dual-gun (one machine, two guns) | Two guns rivet in parallel | Standardized enclosures, cabinet production lines | Two stations, close to double the output |
| Robotic riveting cell | Robot carries the gun along a program and feeds rivets automatically | Battery trays, automotive parts and other high-volume fixed point sets | Unmanned operation, stable cycle time, engineered as a project |
2. Breaking It Down by Feeding and Gun Type
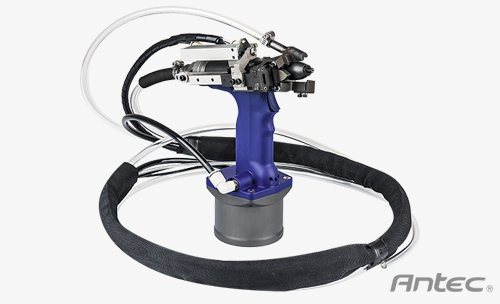
Beyond machine form, the categories also split by process and by feeding design. By process there is the automatic blind rivet machine for blind rivets, the automatic rivet nut gun for rivet nuts, and the automatic rivet gun. By feeding design the common choices are a vibratory bowl feeder, which sorts almost any rivet, and a carousel magazine, which changes over faster and runs quieter. By gun count there are single-gun and dual-gun models. Common Antec models deliver about 12800 N of pull force at roughly 80 cycles/min, with higher pull force and special stroke lengths built to order.
3. Typical Choices by Industry
| Industry | Typical parts | Usual machine choice |
|---|---|---|
| Computer, server and telecom enclosures and cabinets | Case panels, cabinet frames | Handheld gun plus fixed models; dual-gun on volume lines |
| Automotive parts | Interior trim, brackets, assemblies | Dual-gun and robotic cells |
| New energy, lithium battery and solar | Battery trays, structural parts, frames | Mostly robotic riveting cells |
| Sheet metal, power distribution cabinets, appliances and kitchen equipment | Cabinet bodies, housings, brackets | Handheld guns and fixed models |
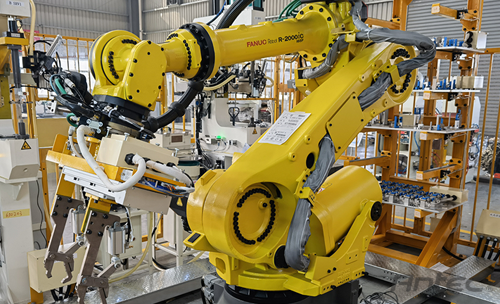
4. Selection and Upgrade Path
Most companies are best served by stepwise automation. Start with a handheld or fixed standard machine to replace manual rivet loading: one machine replaces about 3 workers, and payback commonly runs 2-6 months. As volume and standardization rise, move up to a dual-gun model or a robotic cell, since the same power unit platform scales with you. Match the choice to your own industry, whether automotive parts, electronics enclosures, new energy, sheet metal and power distribution or appliances, and see industry application solutions for detail.
5. Investment and Payback Compared
| Type | Investment level | Payback profile |
|---|---|---|
| Handheld automatic rivet gun | Entry level, lowest investment | Pays back directly on the loading labor it replaces; usually the fastest |
| Bench / fixed | Mid range, including worktable and fixture | Better consistency lifts yield, so payback is steady |
| Dual-gun (one machine, two guns) | Upper mid range | Close to double the output on volume enclosures; the cycle-time math favors it |
| Robotic riveting cell | Project-based investment | Justified by labor savings and unmanned running across the line; best for high-volume dedicated lines |
Note: actual pricing varies with pull force, feeding method and non-standard engineering, so quotes are built from your rivets and workpieces. Payback commonly runs 2-6 months; confirm it against trial data.
6. A Simple Order for Making the Decision
First, the rivet: confirm the type and grip range. Second, the volume: high-mix low-volume work leans toward handheld or fixed models, while high-volume fixed point sets lean toward dual-gun or robotic. Third, budget and stage: prove it with a standard machine, then upgrade in steps. Fourth, close the loop with trial data: run your parts on site, confirm cycle time and yield, then sign. Follow that order and the direction is almost always right.
Machine Type FAQ
Type FAQ
Start with a handheld automatic rivet gun or a bench-style fixed standard machine. Investment is small and results show up fast, and the most labor-heavy step, rivet loading, is automated first.
A dual-gun machine suits standardized parts with two symmetric rows of dense rivet points. When points are scattered or changeovers are frequent, the gain is limited, so compare both on a trial run.
A robotic cell can run as a stand-alone station or be tied into a line. It is normally engineered per workstation and needs your rivet point coordinates and cycle time data.
The differences sit in the feeding mechanism and component grade, machining and assembly accuracy, how thoroughly the machine is run in at the factory, and after-sales parts support. Quote every supplier against the same rivet spec and acceptance standard, then decide on trial results.
Customers Worldwide: Not Sure Which Type? Send Your Parts and We Will Match the Machine
We recommend a handheld, fixed, dual-gun or robotic setup based on your product structure and output. Call +86 13556668682.
Further reading: Automatic blind rivet machine buying guide (full series) · Standard vs. custom machines: how to choose · Riveting solutions for automotive parts
 Previous